
News
EPC Power Distribution Subcontract: How to Control Delivery Risks Prior to Factory Shipment
Reading volume:0 Release time:2026-09-18 08:44:06
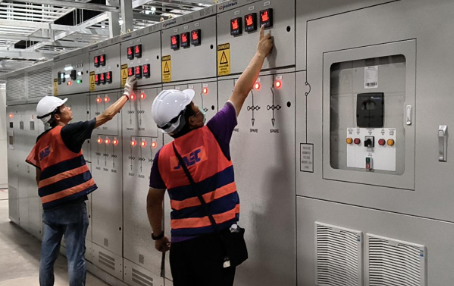
Under the EPC (Engineering, Procurement and Construction) general contracting model, the delivery quality and schedule of power distribution system subcontracts directly affect milestone performance and acceptance costs of the overall project. Risks of power distribution subcontracts in many projects are often fully exposed only during on-site installation, commissioning and acceptance: mismatched goods resulting in substandard performance, dimensional deviations causing on-site rework, and disconnection in production capacity leading to schedule delays. These problems not only raise project costs but also consume coordination efforts of the general contractor. In fact, most on-site risks can be resolved in advance through systematic pre-delivery control.
Three High-Frequency On-site Risks of Power Distribution Subcontracts
1.Mismatched Goods and Performance Deviation
Some subcontractors deliver products with degraded conductor materials, compromised insulation processes, and component parameter deviations, which fail to meet the requirements of the technical agreement. Such defects are highly concealed and usually detected only during on-site tests and final acceptance. They involve long rework cycles and high rectification costs, and in severe cases, directly affect overall project acceptance.
2.Mismatched Interfaces and On-site Rework
Dimensional deviations, inconsistent interface standards and poor plug-in fit of power distribution products are frequent on-site issues. Cutting, modification and repair welding to adapt to site working conditions will not only disrupt construction schedules, but also damage the original structure and protection performance, leaving hidden dangers for long-term operation.
3. Inaccurate Production Scheduling and Schedule Delay
Insufficient capacity assessment, out-of-control production milestones and disconnected logistics coordination by suppliers cause delivery delays against project construction plans. This will affect subsequent procedures including cable laying, equipment installation and system commissioning, and may even trigger liquidated damages risks for the whole project.
Full-process Pre-delivery Control: Closing Risk Loop Within Factory
Risk pre-control represents the most cost-effective management method. Mega Technology has established a full-process control system covering raw materials, production, inspection and shipment. It maximizes control over three core risks: quality, dimension and schedule before delivery to reduce on-site uncertainties.
Three-level Quality Control System: Locking Materials and Processes from the Source
A three-level quality control mechanism of "raw material incoming inspection - in-process milestone inspection - finished product final inspection" is established, with the whole chain aligned with technical agreement requirements:
・Raw material stage: Specifications, material certificates and key parameters of conductors, insulating materials and cabinet plates are verified batch by batch. Batches of core materials are traceable to eliminate material degradation at source.
・Production stage: Quality checkpoints are set for key processes such as insulation forming, cabinet welding and component assembly. Operations are performed in strict accordance with process standards, and each process can only proceed to the next after passing inspection.
・Finished product stage: After each batch is completed, comprehensive inspections on electrical performance, mechanical dimensions and surface protection are carried out item by item to ensure finished products comply with design requirements.
Pre-assembly Verification Before Shipment: Eliminating Interface Installation Risks in Advance
For products such as modular busbars and complete cabinet sets, sectional pre-assembly and interface adaptation verification are completed before shipment. Installation dimensions, connection tolerances and plug-in fit are checked to verify the feasibility and matching of on-site splicing. Dimensional deviations and interface mismatches are identified and rectified in the factory in advance, ensuring direct on-site installation and avoiding rework and quality risks caused by on-site cutting and modification.
Testing by Intertek-accredited Laboratory: Traceable Performance Data
Relying on the company’s Intertek-accredited laboratory, full type tests and pre-shipment sampling tests including temperature rise, power frequency withstand voltage and short-circuit withstand can be performed in accordance with national and international standards. All test data is traceable and reports are verifiable. Consistency between product performance indicators and technical agreements can be validated, preventing performance non-conformities discovered only at on-site acceptance and providing authoritative support for project acceptance.
Standardized Factory Acceptance Test (FAT) Mechanism: Joint Inspection Before Shipment
A standardized customer FAT process is formulated with clear test items, acceptance criteria and judgment rules. EPC general contractors may carry out on-site factory inspection before shipment, verifying product parameters, workmanship quality and bill of configuration item by item against drawings and technical agreements. All identified issues are rectified and closed in the factory prior to delivery, resolving problems before shipment and minimizing on-site rectification costs.
Full-cycle Order Production Scheduling: Securing Delivery Milestones
We have a mature order review and capacity scheduling mechanism. Once an order is confirmed, capacity calculation and milestone breakdown are completed to define timelines for production, inspection and delivery, synchronizing with project progress throughout the whole cycle. Standardized core processes and stable, controllable production capacity effectively avoid schedule delays caused by chaotic scheduling or insufficient capacity, ensuring delivery rhythm matches the overall project construction plan.
Pre-shipment Front-end Control: Three-fold Value for EPC Projects
For EPC general contractors, shifting the control boundary of power distribution subcontracts to the factory side delivers three core values: First, reduce overall on-site costs, cut expenses for on-site rework, modification and coordination, and prevent idle work losses and default risks caused by schedule delays. Second, simplify acceptance closure procedures. Complete original factory test documents and verifiable performance parameters lower communication costs for acceptance and time spent on repeated rectification. Third, clarify quality responsibility boundaries. Product quality status is confirmed before shipment to avoid disputes over liability when on-site defects occur.
High-quality power distribution subcontracting is never a "ship first and deal with issues on site" model. Instead, it features shared risks and process controllability starting from production. Supported by the full-process quality control system, third-party accredited testing capability and standardized delivery mechanism, Mega Technology maximizes containment of quality and schedule risks of power distribution subcontracts before shipment, helping EPC projects achieve controllable quality, schedule and cost.
If you have requirements for power distribution subcontracts for EPC projects, please feel free to contact us for consultation. We provide full-cycle support from solution coordination to pre-shipment delivery.